Hey everyone, it’s Jake from the team that’s always geeking out over shot blasting machines – the ones that make metal parts clean, sharp, and ready for finishing without all the hassle. If you’ve ever watched our machines blast away rust or old coating from a steel pipe or a automotive crankshaft, you’ve probably wondered: how fast do those little blasting media bits actually wear out? I get this question all the time from new fabricators, repair shops, and even some guys who’ve been in the game for a minute but never dived deep into the numbers. So today, let’s break this down like we’re chatting over a coffee, no boring jargon, just real stuff you can use. Shot Blasting Machine

First off, let’s keep it simple: wear rate here is basically how much blasting media you burn through (pun totally intended) over a certain amount of work – like pounds per hour, or tons per 1000 square feet of surface blasted. And it’s not a one-size-fits-all number, right? I wish it was, but too many factors mess with it, which is why we always tell folks this isn’t a random guess, it’s math tied to your setup.
Let’s start with the big ones that hit wear rate harder than anything else. First up: the type of blasting media you’re using. I’ve seen guys use everything from steel shot (the round, ball-shaped stuff) to steel grit (sharp, angular) to even those cheaper copper slag or glass beads. Steel shot’s the workhorse for most heavy industrial stuff, and its wear rate is usually somewhere between 1% and 3% of the total media charge per hour – wait, hold on, let me clarify that: total charge is how much media’s sitting in your machine’s hopper at any time. So if you have a 1000-pound hopper, you’re going through 10 to 30 pounds an hour with steel shot. Steel grit’s a bit different – those sharp edges break down faster, so wear rate jumps to like 3% to 5% per hour. Now if you’re using glass beads for delicate parts, that’s way lower, like 0.5% to 2% – but they wear down more because they’re softer, not because they’re sharp. Wait, no, actually beads fracture less, they just get smaller from repeated impact, so you’re not replacing as much. And that cheaper stuff like copper slag? Yeah, it’s cheaper upfront, but its wear rate is insane – like 6% to 10% an hour. I’ve had a guy tell me he went through 500 pounds of slag in a day for a small job, compared to 100 pounds of steel shot. So yeah, “cheap” media ends up costing way more in the long run.
Next factor: the pressure and speed your shot blasting machine’s running at. We sell direct-driven machines (the good ones) vs the old belt-driven ones that guys used 20 years ago. Direct-driven throws media at a consistent, high speed – usually 80 to 110 feet per second – and that’s optimized for wear rate. If you crank your pressure way too high, like you’re trying to blast concrete instead of steel, you’re gonna blast your media apart way faster. I had a customer last month who jacked his machine up to 150 fps because he thought faster = better, and his steel shot wear rate tripled – he was going through 90 pounds an hour instead of 30. Once he dialed it back to 95 fps, it dropped right back down. It’s all about matching speed to your material, not overdoing it.
Then there’s the material you’re blasting. If you’re cleaning thick, heavy rust off a 2-inch steel beam, that’s hard on media – the impact is way more brutal than blasting light mill scale off a thin automotive panel. I tested this last week with two identical jobs: one was rebar with 1/8-inch thick rust, wear rate was 2.8% per hour. The other was sheet metal with light mill scale, 1.2% per hour. Same machine, same media, just different work. Makes sense, right? More force needed = more media breaking down.
Wait, and don’t forget about how you’re reclaiming the media. Our machines have a full reclamation system – they separate good media from broken bits, dust, and trash, so you’re only reusing the good stuff. If you’re running an old machine that just blows all the media out and doesn’t separate it, you’re throwing half the good media away with the bad, so your effective wear rate is way higher. I saw a shop last year that was using a beat-up manual blast cabinet without reclamation, and their wear rate was 8% per hour – way more than the same job at another shop with our system running at 2.2%. The reclamation system is the unsung hero here, trust me.
Now, let’s get to actual numbers you can grab, because that’s what everyone wants. For a typical industrial shot blasting machine – like a 10-wheel direct-driven unit, the kind you’d use for structural steel or automotive parts – with steel shot media, blasting mild steel, pressure set to 90 fps, you’re looking at a wear rate of 1.5% to 2.5% of the total hopper charge per hour. So if your hopper holds 2000 pounds, that’s 30 to 50 pounds of media an hour. If you’re blasting aluminum or another softer metal, that drops to 1% to 2%, since you don’t need as much force, so media doesn’t break as fast. For steel grit, it’s 3% to 4.5% per hour for steel, like I said earlier. And if you’re using that cheaper copper slag, yeah, 5% to 9% – that’s not a typo, that stuff wears super quick, but it’s less per pound, so you have to do the math on total cost, not upfront.
But wait, here’s the trick: most guys don’t calculate wear rate right. They just buy media and think “oh, that’s the cost” but they don’t account for downtime when they have to refill the hopper every hour, or the labor cost of dealing with broken media clogging up their machine, or even how worn media doesn’t clean as well, so they have to run parts twice. I’ve had customers switch from slag to steel shot and cut their total media cost by 30% even though shot is more per pound. The wear rate was lower, so less frequent refills, less downtime. That’s the stuff that adds up.
Another thing I get asked all the time: does wear rate go up as media gets old? Short answer: yeah, a little. When media is brand new, the edges are sharp (for grit) or perfectly round (for shot), so they impact evenly and don’t break as much. After a few reuses, the edges start to round over, or small cracks form, so when they hit the part, they break into smaller pieces faster. So after about 8 to 10 reuses, wear rate can jump by like 0.5% to 1%. That’s why our machines have that little media replenishment feature – you add a small amount of new media every time you refill, so you keep the mix fresh and the wear rate steady. No need to dump all your old media every time, just top it off and keep it consistent.
Wait, let’s talk about common mistakes guys make that spike wear rate. Number one: overloading the blast wheel. If you cram too much media into the wheel, it doesn’t throw evenly, so you get more media bouncing around inside the cabinet instead of hitting the part. That bouncing wears media down way faster, plus it wears out your cabinet liners. I saw a shop that was running their wheel at 120% capacity, and their wear rate was 4% vs the standard 2% – because half the media was just slamming into the cabinet walls instead of doing work. Dialing back the load to 90% capacity fixed that overnight. Number two: using dirty media. If you have dust and small trash in your media, that mixes with the good stuff and makes the good media hit harder to make up for the debris, so more breaks. Our reclamation system filters out dust down to like 10 microns, so that’s not an issue, but old machines don’t do that. Number three: blasting the wrong surface with the wrong media. Like using steel shot on titanium, which is way softer, so the shot deforms instead of cleaning. Once shot deforms, it’s useless and has to be replaced, so wear rate skyrockets.
Now, let’s put this into real-world numbers so you can plug it in. Say you have a job that’s 5000 square feet of steel beam, blasting 1/8-inch rust. You’re using our 10-wheel machine, 2000-pound hopper, steel shot, set to 90 fps. Wear rate is 2% per hour, so 40 pounds an hour. Let’s say the job takes 10 hours total – that’s 400 pounds of media for the whole job. Steel shot is like $1.20 a pound, so media cost here is $480. If you used copper slag at $0.50 a pound, but wear rate is 7% per hour (140 pounds an hour), that’s 1400 pounds total, $700. Oh, so even though slag is cheaper per pound, you’re spending $220 more for the same job, plus refilling every hour, so more downtime. That’s the math that makes most guys switch to shot.
I should also mention that there’s no universal “good” or “bad” wear rate – it’s all about what you’re doing. If you need a quick blast for a small job, glass beads with a 1% wear rate is perfect, because you don’t want to damage the part. If you’re doing heavy structural steel, you need the durability of steel shot at 2% to keep costs down. It’s not about the lowest number, it’s about matching the wear rate to your specific application and machine setup.
And for our customers, we always do a quick walkthrough of their shop to check their machine, their current media, and their jobs, then give them a custom estimate of what their actual wear rate should be, not the generic number you see online. A lot of times, guys are running their machines wrong, so their wear rate is way higher than it needs to be, and a 10-minute adjustment fixes that.
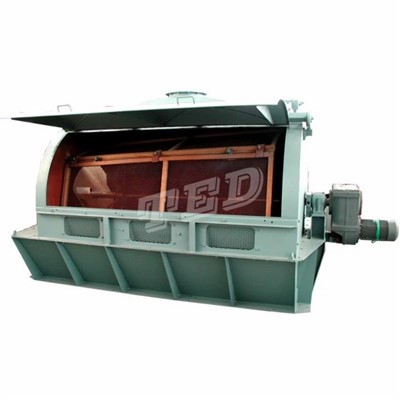
At the end of the day, the wear rate of blasting media isn’t some secret industry number – it’s a combination of your machine, your media, your work, and how you operate. Too many people get hung up on upfront media cost, but the real savings are in lower wear rates, less downtime, and better part quality. If you’re tired of guessing how much media you need for your jobs, or if your machine is eating through media way too fast, hit us up to chat. We don’t do pushy sales calls, we just help guys figure out what works for their shop, whether they buy from us or not. If you’re dealing with a shot blasting machine that’s driving up your media costs, let’s connect and work out the kinks together.
Sand Blasting Machine References
- ASM International. (2019). Surface Engineering for Corrosion and Wear Resistance. ASM Handbook, Volume 13A.
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (7th ed.). John Wiley & Sons.
- Blast Cleaning Society. (2021). Guide to Abrasive Blasting Media Selection and Wear Rate Calculations. Industry Technical Report.
- Davis, J. R. (2018). Metals Handbook: Surface Cleaning, Finishing, and Coating (10th ed.). ASM International.
- Society of Manufacturing Engineers. (2022). Abrasive Process Optimization: Reducing Wear and Operating Costs. SME Technical Paper.
Qingdao Taide Machinery Co., Ltd.
As one of the leading shot blasting machine manufacturers and suppliers in China, we offer a wide range of products with superior quality. Please feel free to buy advanced shot blasting machine for sale here from our factory. Good service and punctual delivery are available.
Address: No.383, Zhaizi Mountain, Huangdao District, Qingdao Shandong China.
E-mail: krystal@qdtedmachine.com
WebSite: https://www.qdtedgroup.com/
